Alright, let’s cut to the chase—if you’re a metal fabricator or a pipe shop owner, you’ve probably asked this question at some point: Can my steel pipe processing equipment handle titanium pipes? As someone who’s spent the last decade selling steel pipe processing machines (think not just cutters, but bevelers, end prep units, and even the occasional edging system), I get why this is top of mind. Titanium is sexy right now—everybody’s using it for aerospace, medical parts, even high-end bike frames—but it’s also weirdly finicky. You don’t wanna ruin a $500 titanium pipe with a cutter you use for cheap steel, right? Let’s break this down like I’m explaining it to a buddy who’s staring down a bunch of titanium stock and a used pipe notcher he’s had in the back of his shop. Steel Pipe Processing Equipment
First, let’s start with the basics: why steel machines can work for titanium… if you tweak a few things. Wait, before you get too excited or too stressed, let’s define what “steel pipe processing equipment” usually means for most small to mid-sized shops. It’s generally not the giant automated lines you see at heavy mills—those are for bulk steel, so they’re built for speed, not precision with soft, scratch-prone metals. The stuff I sell is the mid-range, versatile stuff: manual and semi-automatic cutoff saws (both abrasive and cold saw types), portable bevelers for end prep, pipe end facing machines, and maybe a little roller for bending small-diameter pipes. That’s the sweet spot where a lot of folks overlap steel and titanium work.
Let’s get into the metal properties here, ‘cause that’s the make-or-break. Titanium has a tensile strength that’s actually similar to some high-strength alloy steels (like 4130), but it’s way softer than tool steel, and way more ductile. Wait, no—wait, hold on, let’s not mix that up: pure titanium is soft, like commercially pure (CP) grades, which are used for fittings and general parts. The alloyed titanium (Ti-6Al-4V, the workhorse) is stronger, but still not as hard as, say, 1045 steel. The problem isn’t strength—it’s two other things: thermal conductivity and work hardening. Steel has high thermal conductivity, right? It absorbs heat fast, so when you cut it, the heat goes into the chip and doesn’t mess with the pipe. Titanium? It’s like 1/5 as conductive as steel. So when you cut it, all that heat stays right at the cutting edge, which melts the titanium and makes it gum up on your saw blades, like when you try to cut plastic with a dull knife. Also, titanium work hardens super easy—meaning if you’re pushing too hard, the surface gets harder, and the next cut just tears it, leaving a rough edge or scratches that you can’t buff out.
Okay, so now tie that to the machines I sell. Let’s take cutoff saws first. A lot of my customers use their steel cold saws for titanium all the time—if they swap the blade. Steel saw blades have carbide tips that are designed for high speed, but for titanium, you need a blade with more teeth, right? Wait, no—actually, a higher tooth count per inch (TPI) blade, but a more flexible blade that doesn’t dig in. Oh, and coolant is non-negotiable. For steel, you might use a generic soluble oil, but for titanium, you need a synthetic coolant that’s formulated to stick to the surface and reduce friction, not just wash away heat. I’ve had guys show up at my shop with a $2k cold saw they bought from me 6 months prior, asking if they can use it for titanium, and the first thing I ask is: “Do you have coolant lines that direct right at the cut, not just a mist?” If they do, and they swap the blade, it works. The abrasive saws? Yeah, those work too, but only for rough cuts—they’ll leave a really rough edge, and you’ll have to grind off a ton of material, which is wasteful for titanium. I always tell people: if you need a clean, precise cut for welding or machining, stick to the cold saws from my line.
Next up, beveling machines—another big part of steel pipe processing that’s used for titanium all the time. Most pipe bevelers I sell are portable, electric, and adjustable, so you can set the angle for 30-degree bevels for welding, which is exactly what you need for titanium pipes. The key here is the cutting tool for the beveler. For steel, you might use a high-speed steel (HSS) tool bit, but for titanium, you need a carbide-tipped bit with a positive rake angle. Wait, what’s a positive rake? It just means the edge is angled to shear the material instead of tearing it, which is perfect for soft, ductile titanium. Also, when beveling titanium, you can’t push as hard as you would for steel. A lot of guys crank the handle on their steel beveler, and that’s where they mess up titanium—they work harden the surface so bad that the tool just slides off instead of cutting. I tell ‘em: light, steady pressure, like you’re cutting a carrot, not a steel rod. That’s the trick.
End facing machines, too—those are super common for steel pipes to get a flat, smooth end for threading or fitting. They work for titanium no problem, ‘cause end facing is a shallow cut, right? No heavy pressure, the tool just skims the surface. Again, just swap the tool bit if needed, use some coolant, and you’re good to go. I had a customer last year who used my end facing machine to prep 2-inch titanium pipes for medical implants—he just used a carbide bit and slow speed, and got a surface finish so smooth he didn’t have to buff it. Saved him a ton of time.
Now, let’s talk about when it won’t work. This is important, ‘cause I don’t wanna sell you a machine and have you come back mad. If your steel pipe processing equipment is a beat-up old manual cutter that doesn’t have any speed control, that’s a problem. Titanium needs lower cutting speeds than steel—like, for a cold saw, steel might cut at 100 feet per minute (FPM), titanium is more like 30-50 FPM. If your machine only goes fast, you’ll burn through the blade, ruin the pipe, and make a huge mess. Also, if your machine has loose parts, or a saw blade that’s wobbling, that’s bad for titanium— it’ll leave uneven cuts, cause work hardening, and scratch the surface, which is a big deal for titanium that’s gonna be used for something like a bike frame or aerospace part where surface integrity matters.
Another thing people forget: clamping. When you cut steel, a vise or a pipe clamp is enough, but titanium is soft, so if you clamp it too tight, you’ll leave indentations that you can’t get out. And if you use steel clamps without any padding, you’ll scratch the titanium, which is a defect. I always recommend using rubber or copper padding on your clamps when running titanium through the machines I sell. It’s a $20 fix, but it saves you from scrapping a $300 pipe.
Wait, let’s talk about common mistakes I see. Last month, a guy brought his steel pipe notcher to my shop, trying to notch 1-inch titanium pipes for a custom exhaust. He was using the same abrasive wheel he uses for steel, cranking the speed all the way up. I watched him cut a test piece, and within 10 seconds, the wheel started gumming up with titanium chips, the pipe was burning, and he had a notch that was way too big. I showed him to swap to a cold saw blade with 18 TPI, slow the speed down to 40 FPM, use synthetic coolant, and pad the vise. The next day, he came back with the finished notches, and they were perfect—no burn, no work hardening, fit exactly where he needed it. That’s the difference between winging it and actually understanding how the equipment works with titanium.
Now, should you invest in dedicated titanium equipment? That’s a fair question. If you’re only gonna cut 1 or 2 titanium pipes a month, just tweak your existing steel machines—swap blades, use coolant, adjust speed. But if you’re running a lot of titanium, say 10+ pipes a week, then you might wanna upgrade to a machine that’s built specifically for titanium, like a saw with variable speed control, or a beveler with a closed-loop coolant system. But the nice thing about the steel processing equipment I sell is that it’s versatile—you can run steel all day, and then switch to titanium with just a few quick adjustments, no need for two separate lines. That saves you money, which is huge for small shops.
Let’s also address safety, ‘cause titanium isn’t as scary as some people make it, but you still gotta be careful. When you cut it, the chips are sharp, and they can get hot. For steel chips, you might not think twice, but titanium chips can ignite if they’re fine and get exposed to a lot of heat. So always wear safety glasses, gloves, and a face shield when cutting titanium, same as you would for steel. And never leave loose titanium chips sitting around in a pile—dispose of them properly, ‘cause they can be a fire hazard. I’ve had a customer who forgot to clean up his titanium chips, and when he turned on his dust collector, the chips ignited, and he had a small fire in his shop. Not fun.
Wait, let’s circle back to the original question, ‘cause I know you’re here for a clear answer. Yes, your steel pipe processing equipment can be used for titanium pipes—if you make a few key adjustments. The biggest ones are: swap to the right blades/tool bits, lower the cutting speed, use the right coolant, pad your clamps, and use light, steady pressure. That’s it. You don’t need to go out and buy a whole new $100k line of titanium-specific machines (unless you’re doing huge volume). The mid-range steel processing equipment I sell is built to be flexible, so it works for both common steel and more specialized metals like titanium.
Now, if you’re sitting there right now with titanium stock and a steel pipe cutter that’s been sitting in your shop, don’t overcomplicate it. First, check your machine: does it have variable speed? Do you have coolant lines? If yes, you’re 90% there. If not, we can add those upgrades too—nothing’s too custom. If you’ve tried running titanium through your steel machine before and it didn’t work, that’s probably ‘cause you skipped one of those adjustments, not ‘cause the machine is bad.
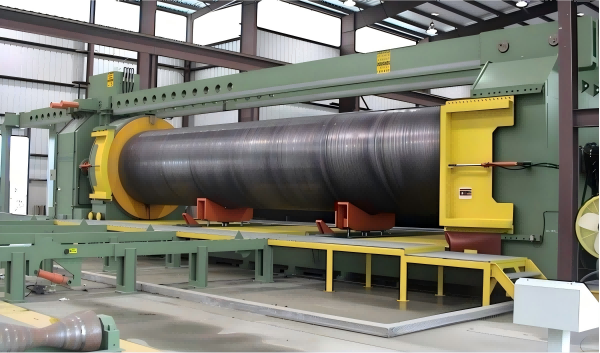
At the end of the day, this is what I love about my job—helping guys get the most out of their existing equipment without wasting money on stuff they don’t need. If you’re curious about how to adjust your steel pipe processing machine for titanium, or you’re looking to upgrade to something that’s easy to switch between steel and titanium, hit me up. No pressure, just a chat to figure out what works for your shop.
Pipe-making Machinery Spare Parts References:
- ASM International. (2005). Properties and Selection: Nonferrous Alloys and Special-Purpose Materials. ASM Handbook Volume 2.
- Machining Data Handbook. (2020). 11th Edition. Modern Machine Shop Publications Inc.
- Titanium Metal Fabrication Guidelines. (2018). International Titanium Association.
- Pipe Processing Equipment: Versatility for Mixed Metal Shops. (2022). Fabricating & Metalworking Magazine.
Tianjin Binhai Yashanway Import and Export Co., Ltd.
Tianjin Binhai Yashanway Import and Export Co., Ltd. is one of the most reliable steel pipe processing equipment manufacturers and suppliers in China, also supports customized service with low price. Welcome to wholesale bulk steel pipe processing equipment made in China here from our factory. Contact us for quotation.
Address: B-508, Xiangnian Plaza, Dongjiang Road, Hexi District, Tianjin, China
E-mail: crystal@yashanway.com
WebSite: https://www.yashanway.com/
